.png)
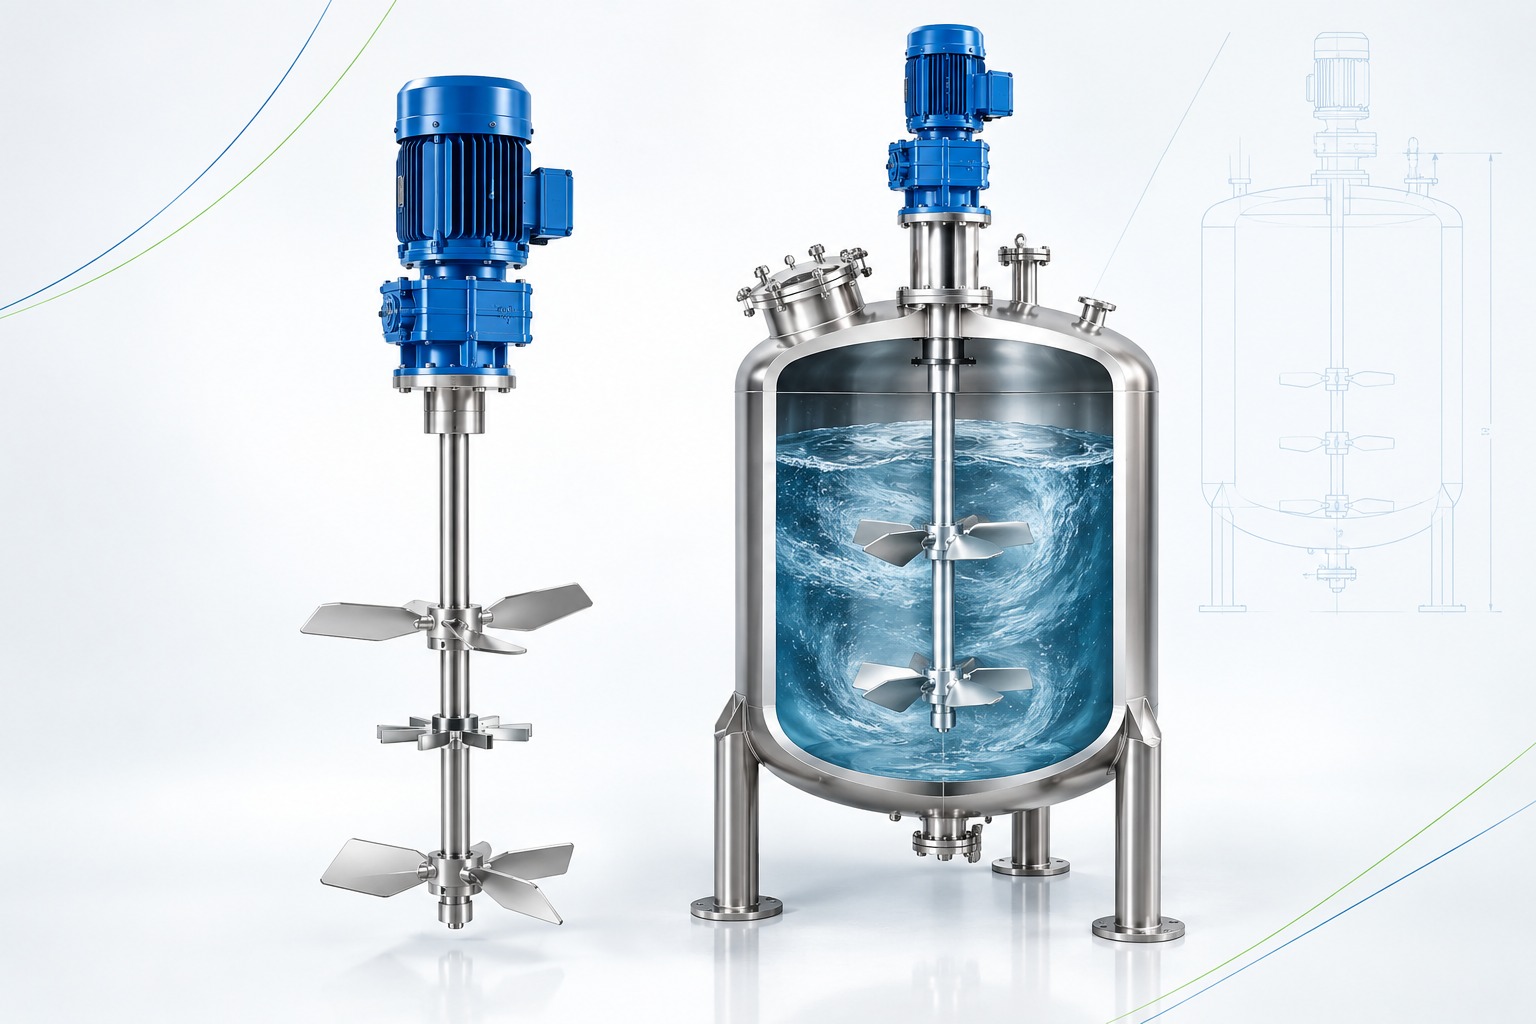
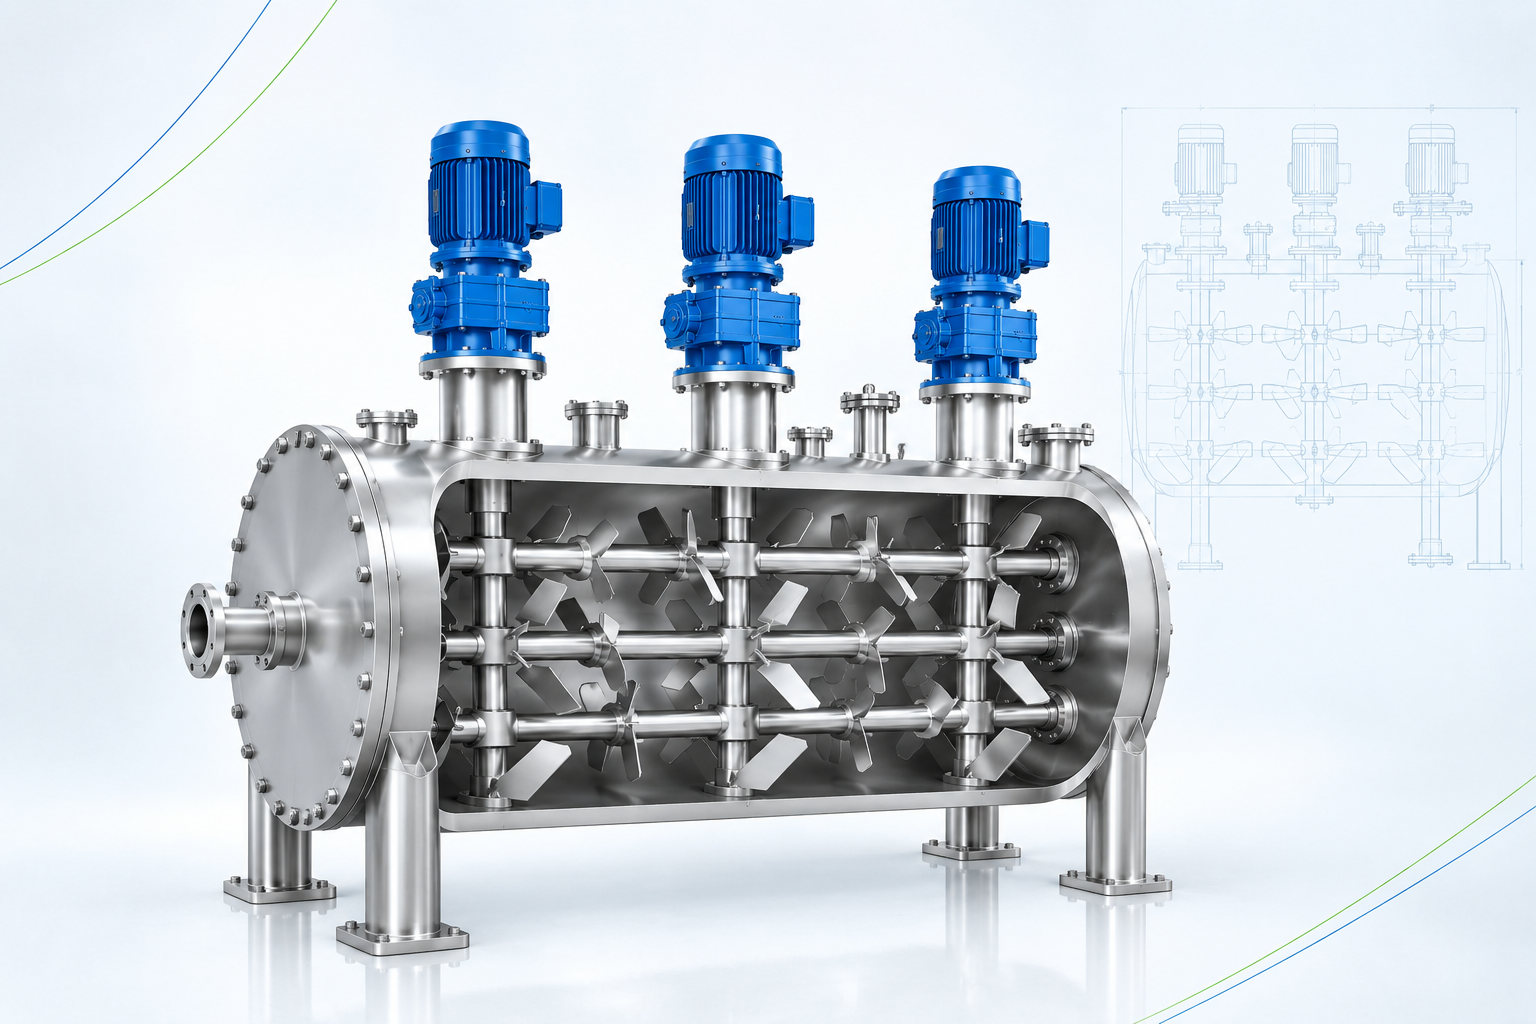
Multi-Axial (Triple Shaft) Agitators
we are proud to offer our cutting-edge Multi-Axial Agitator (Triple Shaft Agitator), designed for versatile, high-performance mixing in a wide range of industrial applications. This advanced agitator system combines the functionalities of three individual shafts, providing superior mixing efficiency for highly viscous, complex, and diverse materials. It is ideal for industries such as chemicals, adhesives, sealants, coatings, and inks, where precise, consistent mixing is critical.
Get Your Free Quote…!
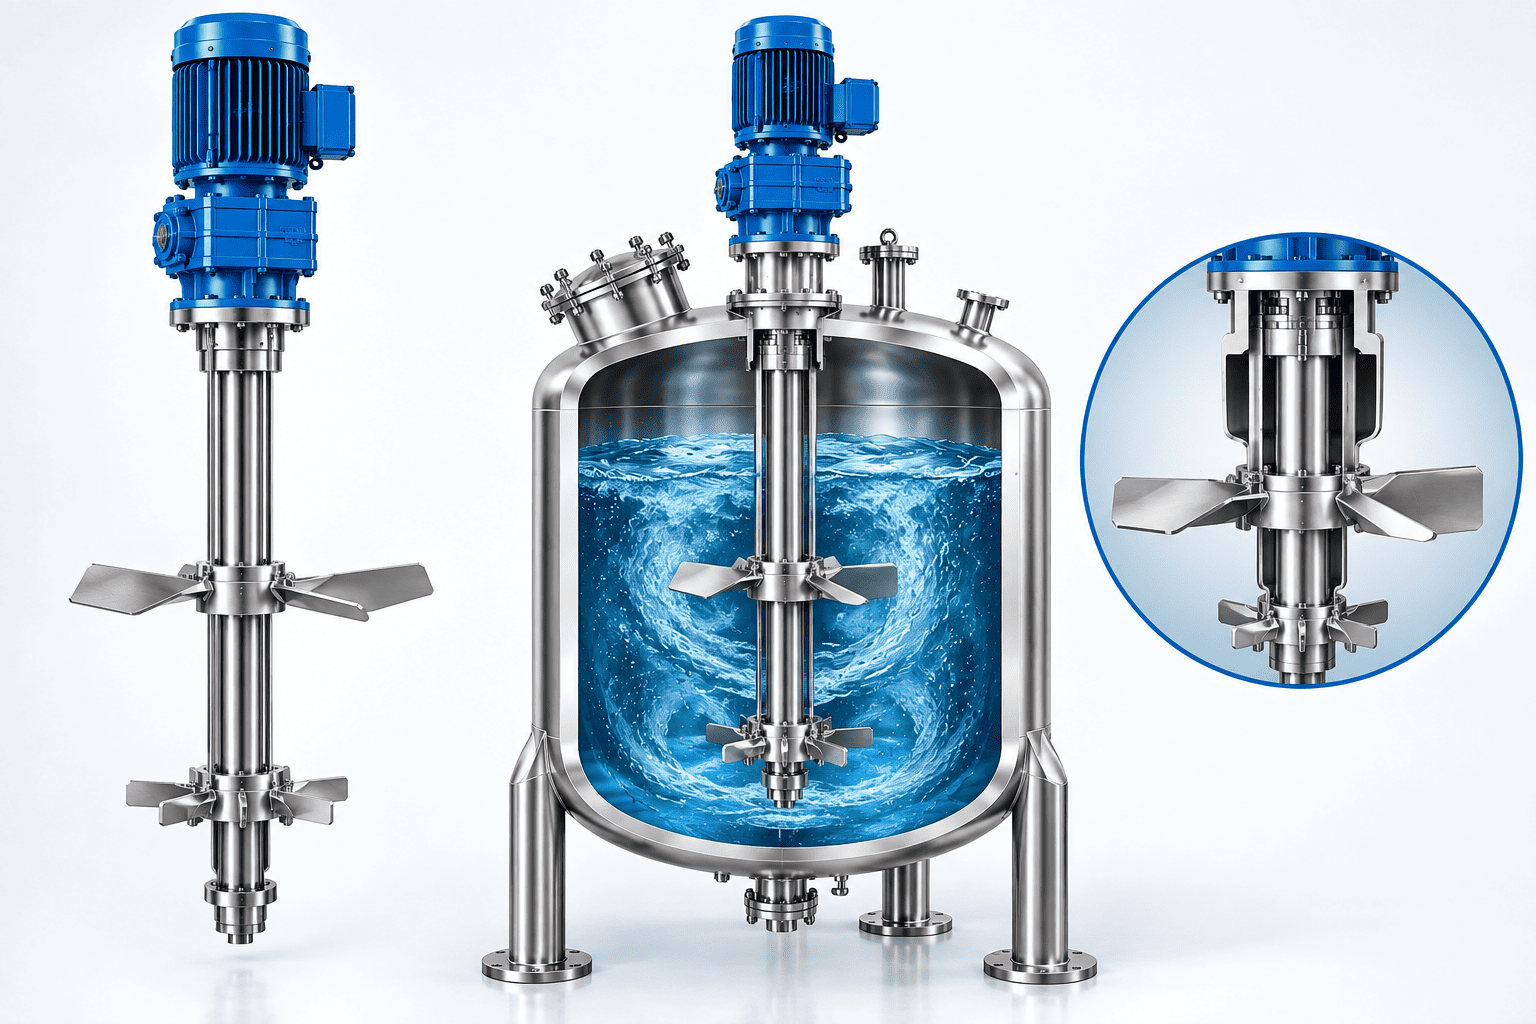
Coaxial Agitator
we redefine mixing technology with our state-of-the-art Coaxial Agitators. Engineered for the most demanding applications, our coaxial design integrates two independently driven agitators on a single axis, delivering unparalleled control and versatility. This innovative dual-action system is the definitive solution for complex processes involving high-viscosity fluids, delicate suspensions, and challenging homogenization tasks where a single agitator falls short.
Our Coaxial Agitators provide a unique synergy of low-speed, high-torque bulk movement and high-speed, high-shear dispersion, ensuring perfect product consistency every time.
Get Your Free Quote…!
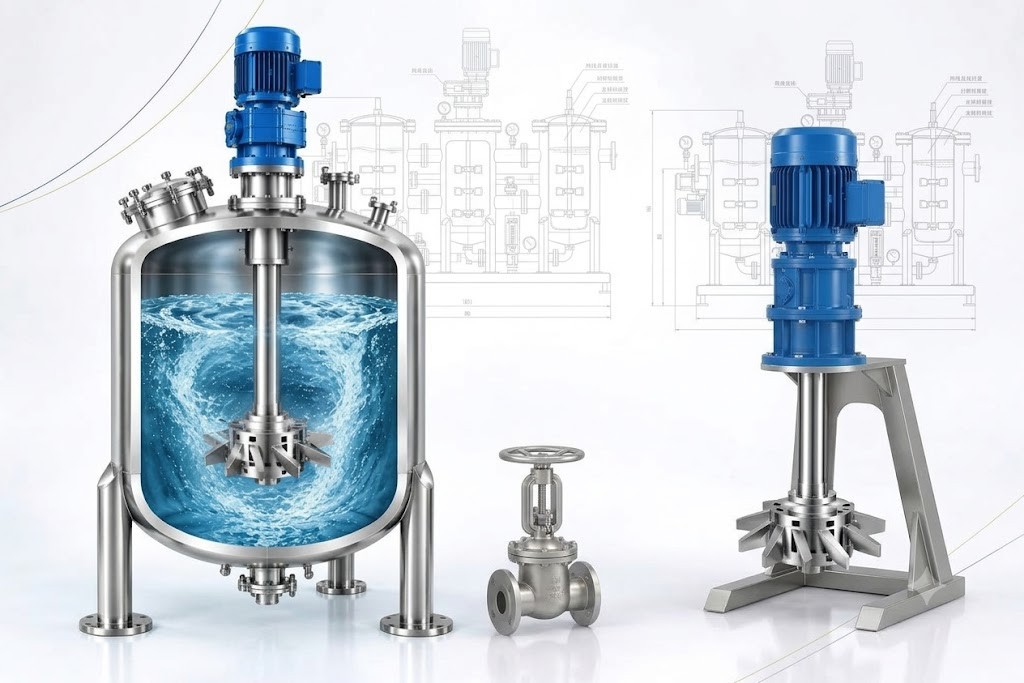
Chemical Reactor Agitator
we understand the critical role agitation plays in ensuring efficient and successful chemical reactions. As a leading manufacturer of chemical reactor agitators, we are committed to providing solutions that optimize your processes and maximize your yields within the demanding world of chemical production.
Get Your Free Quote…!
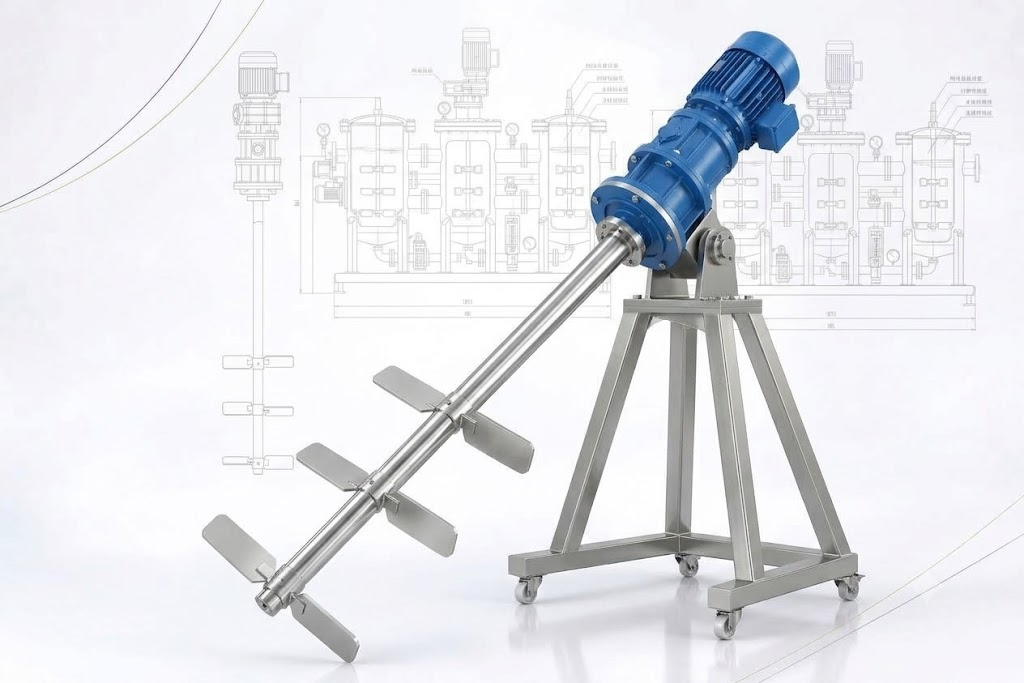
Long Shaft Paddle Agitator for Biogas Plant
We make Side Entry Long Shaft Paddle Agitator is specially designed for Biogas and CBG plants to handle high viscosity, fibrous, and high solids (TS) substrates efficiently.
The agitator operates on a low speed – high torque principle, ensuring gentle yet effective mixing without disturbing biological activity inside the digester.
Widely used in:
Primary Digesters
Secondary Digesters
Digestate Storage Tanks
The long shaft with multiple paddles ensures complete top-to-bottom mixing,
preventing floating layers and sedimentation.
Get Your Free Quote…!
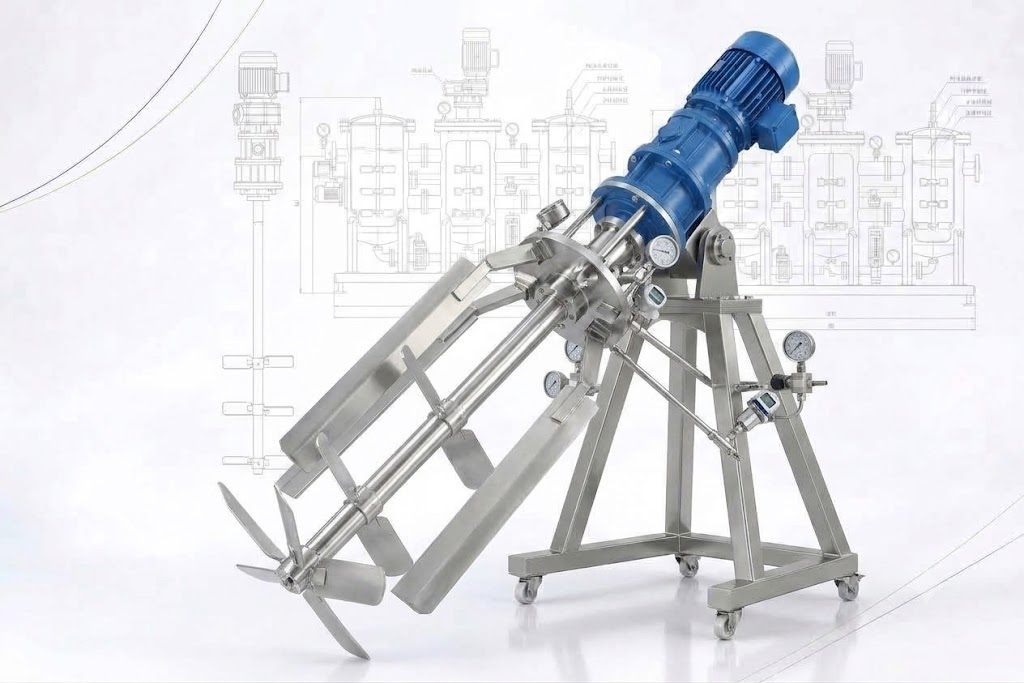
Central Mixer for Biogas Digesters
Our Central Mixer Agitator is designed for installation at the center of biogas digester tanks to ensure uniform mixing, improved gas yield, and stable long-term operation.
Get Your Free Quote…!
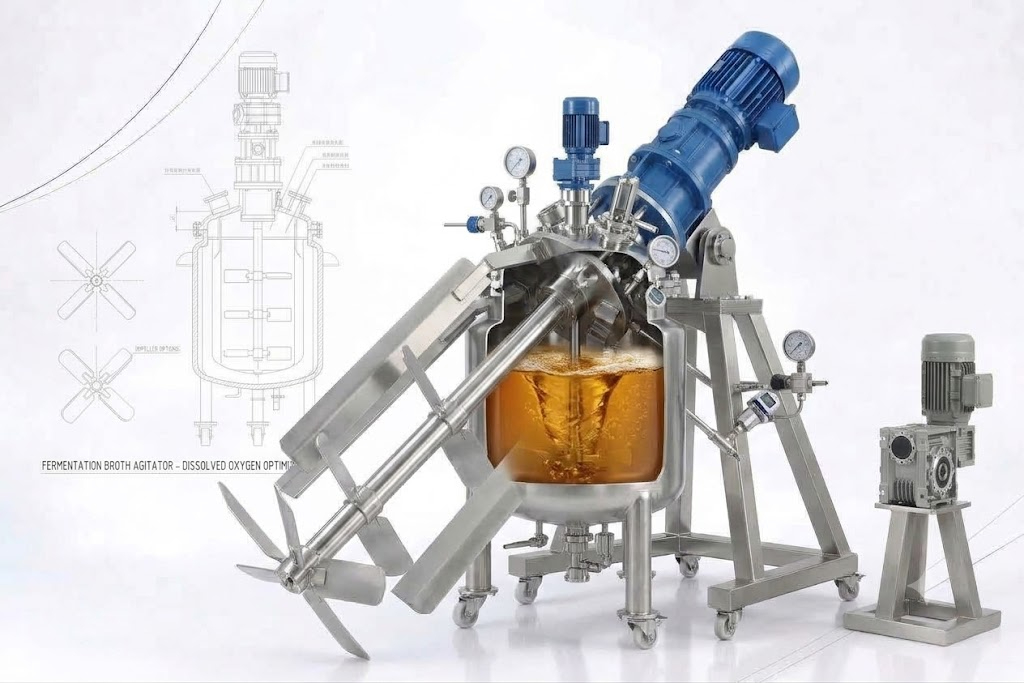
Fermentation Broth Agitator
Fermentation is a critical process in industries such as pharmaceuticals, biotechnology, food & beverage, and biofuels. The Fermentation Broth Agitator is an essential component that ensures uniform mixing, optimal aeration, and efficient mass transfer, leading to enhanced microbial and enzymatic activity.
We offer cutting-edge Fermentation Broth Agitators designed to optimize process performance, from lab-scale development to full-scale production. Our solutions are tailored to meet the most stringent industry standards, ensuring high efficiency, energy savings, and regulatory compliance.
Get Your Free Quote…!
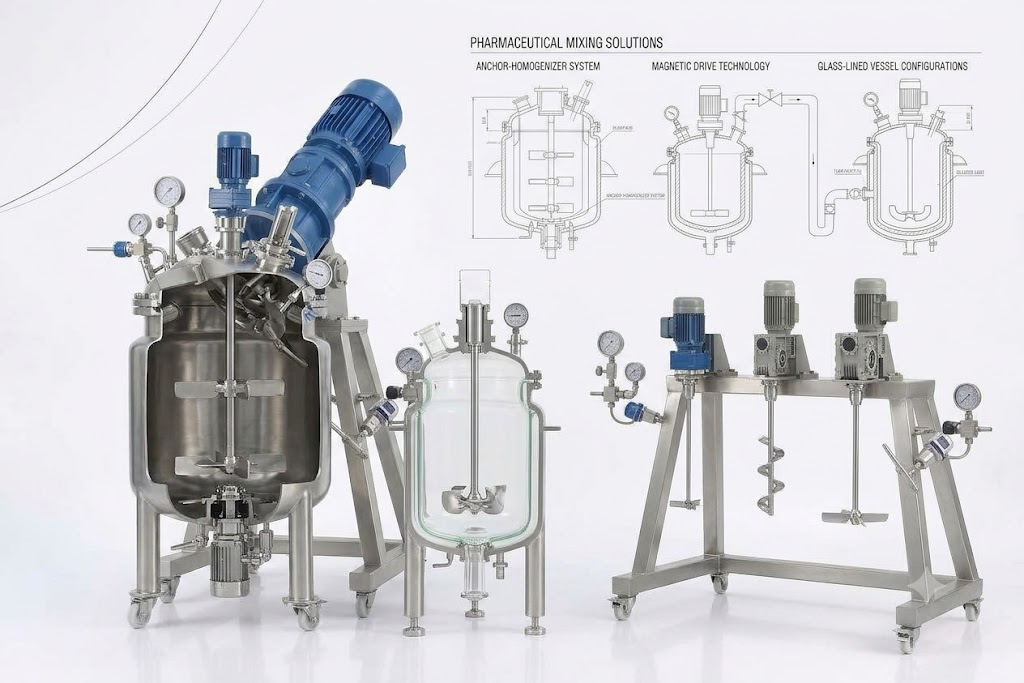
Agitators for Pharmaceutical Industry
We specializes in the design and manufacture of high-performance agitators tailored to meet the stringent requirements of the pharmaceutical industry. Our agitators are engineered to provide precise, reliable, and contamination-free mixing solutions, ensuring that the most delicate pharmaceutical processes are conducted with efficiency and safety. Whether used in small-scale laboratory settings or full-scale production environments,
Our agitators are built to deliver superior performance, ensuring consistency, repeatability, and compliance with the highest industry standards.
Get Your Free Quote…!
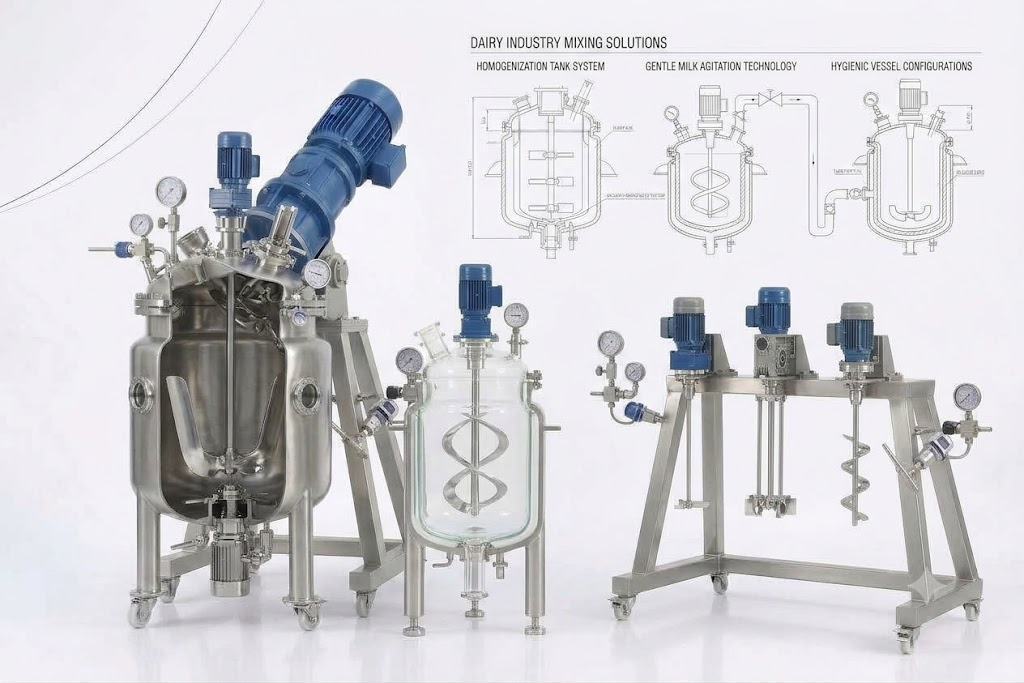
Agitators for Dairy Industry
We are global leader in the design and manufacturing of high-performance agitators specifically tailored for the dairy industry. Our innovative solutions are engineered to meet the unique challenges and demands of dairy processing, ensuring optimal mixing, product consistency, and overall operational efficiency.
Our agitators are designed with precision to meet the strict hygiene and quality standards required in dairy production
Get Your Free Quote…!
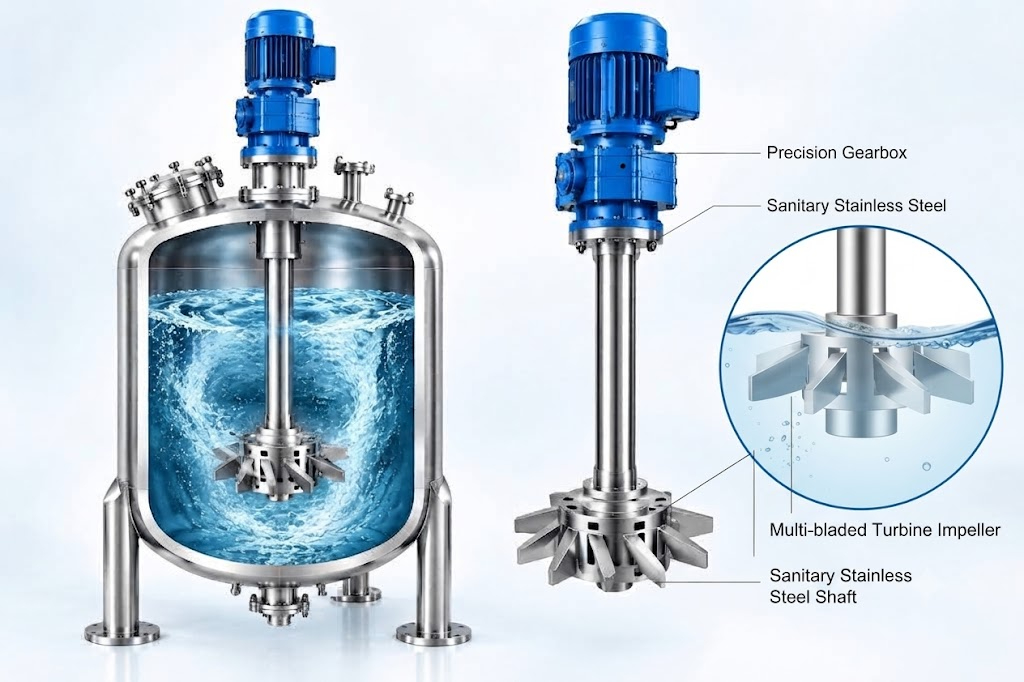
Agitator for Distillery Fermentation Tanks
Fermentation is a critical stage in the distillation process, where yeast converts sugars into alcohol. Efficient mixing within the fermentation tank is essential for optimal yeast growth and alcohol production. Our distillery-specific agitators are designed to deliver superior performance and reliability, ensuring consistent and efficient fermentation.
Get Your Free Quote…!
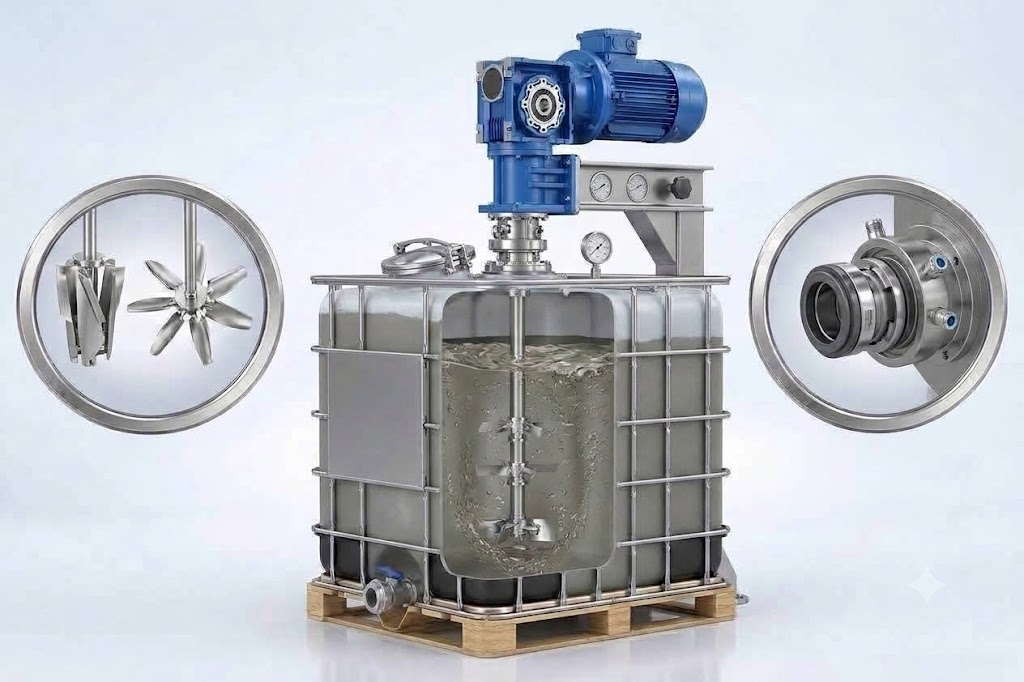
Mineral Slurry Agitator
Agitators are a trusted choice for mining projects around the world. Our commitment to innovation extends to cutting-edge impeller technology and design methodologies. These advancements have yielded significant improvements in agitator performance and overall leaching process efficiency.
We meticulously analyze factors like particle size, Solid Concentration, density, and flow rate to design impellers that perfectly match your specific process requirements. Moreover, the mechanical robustness of our agitator components and drive systems is meticulously engineered to deliver both cost-effectiveness and resilience.
As a leading global manufacturer of heavy-duty agitators, Verito sets the standard for quality, reliability, and performance in the mining industry. Each Verito agitator is custom-designed by our team of highly trained and experienced design engineers to meet your specific needs and process requirements. Let Verito be your partner in achieving optimal results in your next mining project.
Get Your Free Quote…!
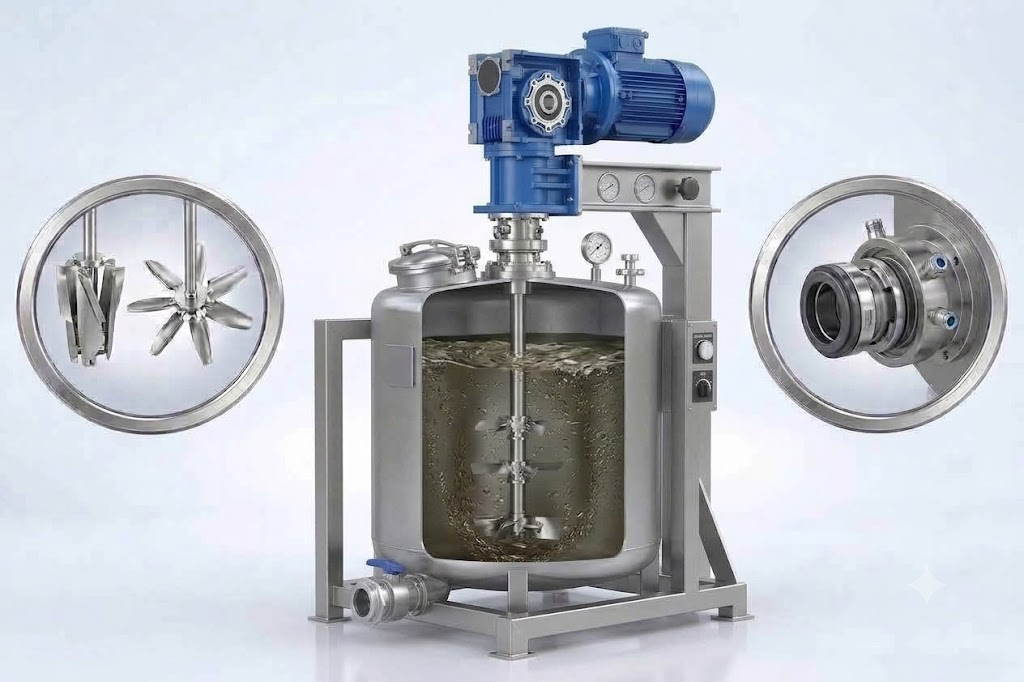
Flue Gas Desulfurization (FGD) Agitator
we pride ourselves on being at the forefront of engineering excellence, delivering high-performance Flue Gas Desulfurization (FGD) agitators that stand as a benchmark in the industry. Our commitment to quality, innovation, and environmental sustainability drives us to create agitators that not only meet but exceed the rigorous demands of modern industrial processes.
Get Your Free Quote…!
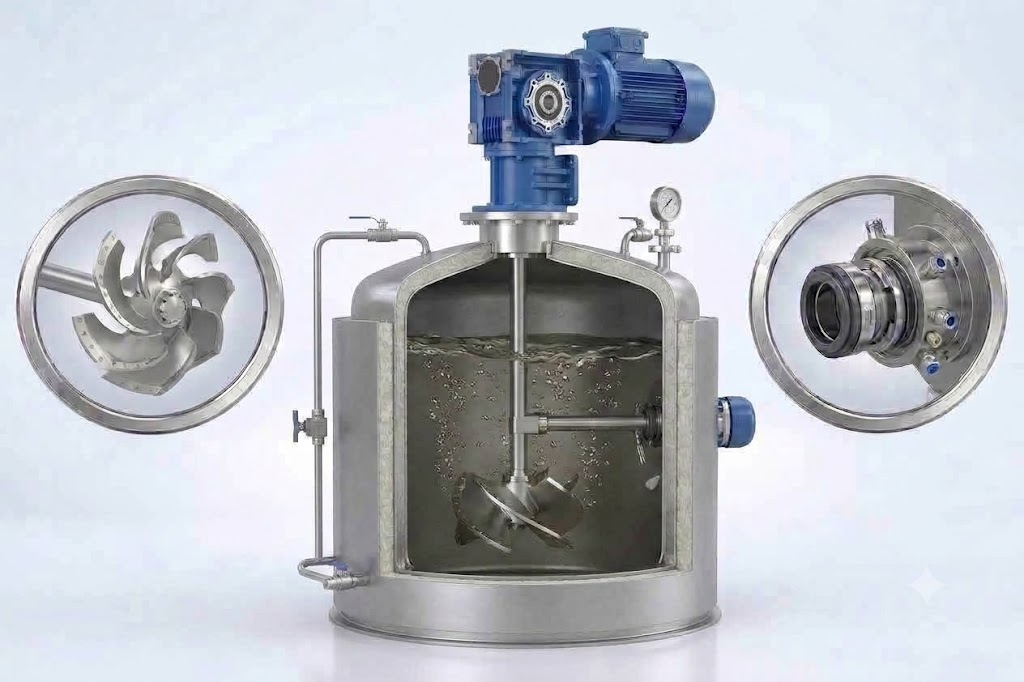
Side Entry Agitator for Digestor Tank (Bio Gas Plant)
The forefront of innovation in the design and manufacture of side entry agitators, specifically tailored for biogas plant digestor tanks. Our agitators are engineered to meet the rigorous demands of biogas production, where the efficiency of organic material digestion directly impacts gas yield and overall plant performance. With a commitment to quality, precision, and durability, Verito’s side entry agitators are the ideal solution for optimizing the mixing process within digestor tanks, ensuring consistent and reliable biogas production.
Get Your Free Quote…!
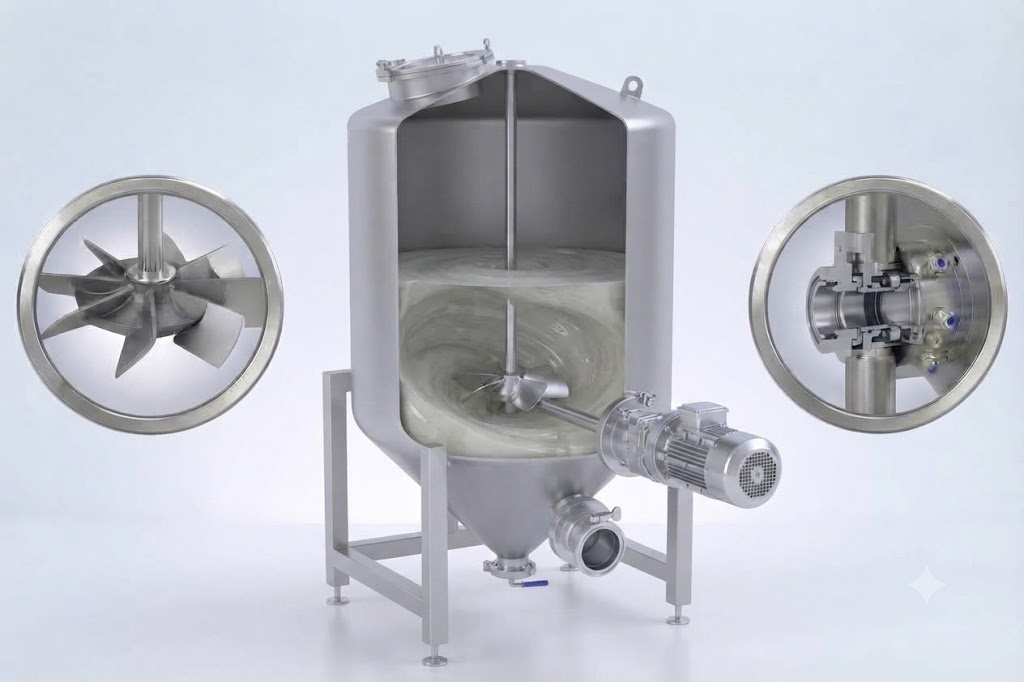
Side Entry Agitator for Food-Processing Storage Tanks
We proudly offers a highly engineered solution for efficient agitation in large-volume food-processing storage tanks, specifically designed for low viscosity products like wine, oil, milk, beer, alcohol, and similar fluids. Our side entry agitators are built to deliver consistent and uniform mixing, ensuring optimal product quality, minimal energy consumption, and extended shelf life.
Get Your Free Quote…!
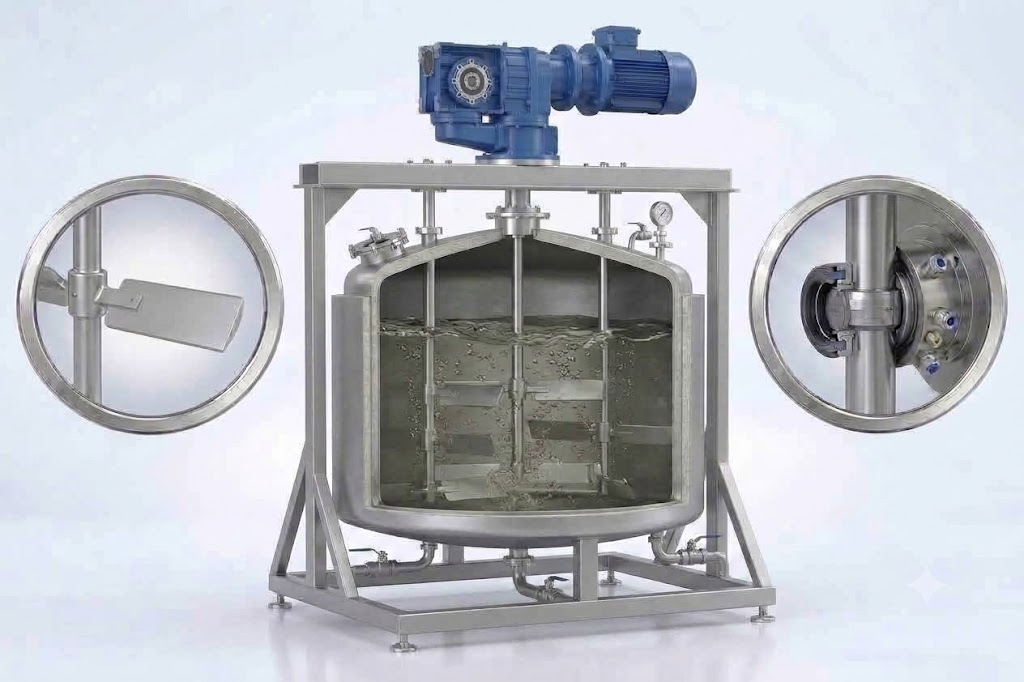
Paddle Flocculator
A Paddle Flocculator is a key piece of equipment used in water and wastewater treatment processes to promote flocculation – the gentle mixing of coagulated particles to form larger aggregates (flocs) that can be easily separated through sedimentation or filtration. Designed for optimal energy efficiency, uniform mixing, and controlled shear, paddle flocculators are widely used in municipal, industrial, and process water treatment applications.
We offer robust, efficient, and customizable paddle flocculators engineered for reliable operation under varying process conditions. Our designs focus on performance, durability, ease of maintenance, and energy optimization.
Get Your Free Quote…!
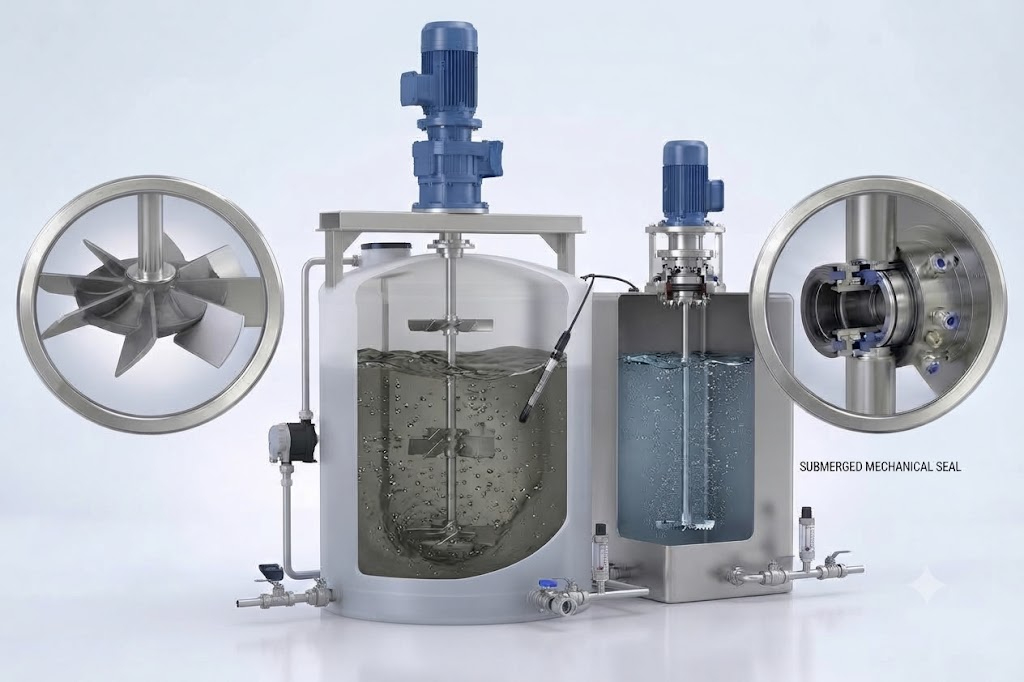
Agitators for Water Treatment & Dosing Tanks
we specialize in designing high-performance agitators for Water Treatment Dosing Tanks, engineered to meet the complex demands of various water treatment processes, including Water Treatment Plants (WTP), Wastewater Treatment Plants (WWTP), Sewage Treatment Plants (STP), Effluent Treatment Plants (ETP), and Desalination projects. Our agitators ensure the effective mixing of chemicals and slurries to maintain precise dosing levels for optimal water quality.
Get Your Free Quote…!
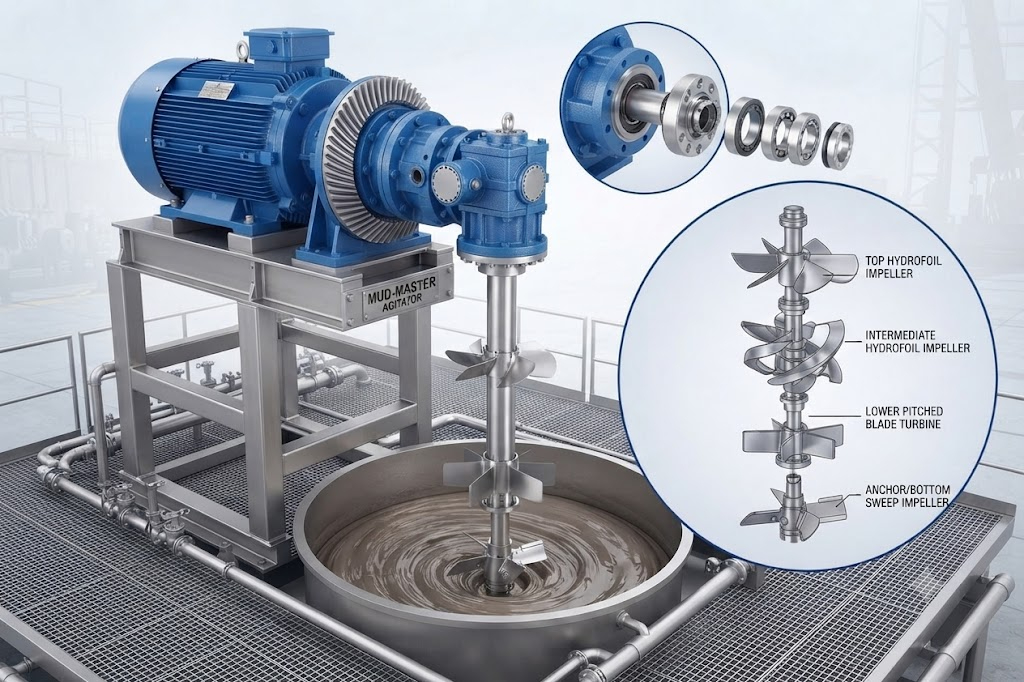
Mud Agitators for Drilling Fluids in Oil & Gas Operations
we design and manufacture Mud Agitators specifically tailored for the oil & gas, mining, and drilling industries. Our agitators play a crucial role in maintaining the homogeneity of drilling fluids, preventing the settlement of solids, and ensuring efficient mud circulation in mud tanks. Built to handle the demanding requirements of these industries, our agitators are engineered to deliver high-performance mixing even in the harshest environments.
Mud agitators are essential for the proper management of drilling fluids (drilling mud). These fluids are critical to the drilling process, providing cooling, lubrication, and stabilizing pressure. Verito Engineering’s Mud Agitators ensure the effective suspension of solid particles in the drilling fluid, thereby enhancing operational efficiency and extending equipment life.
Get Your Free Quote…!
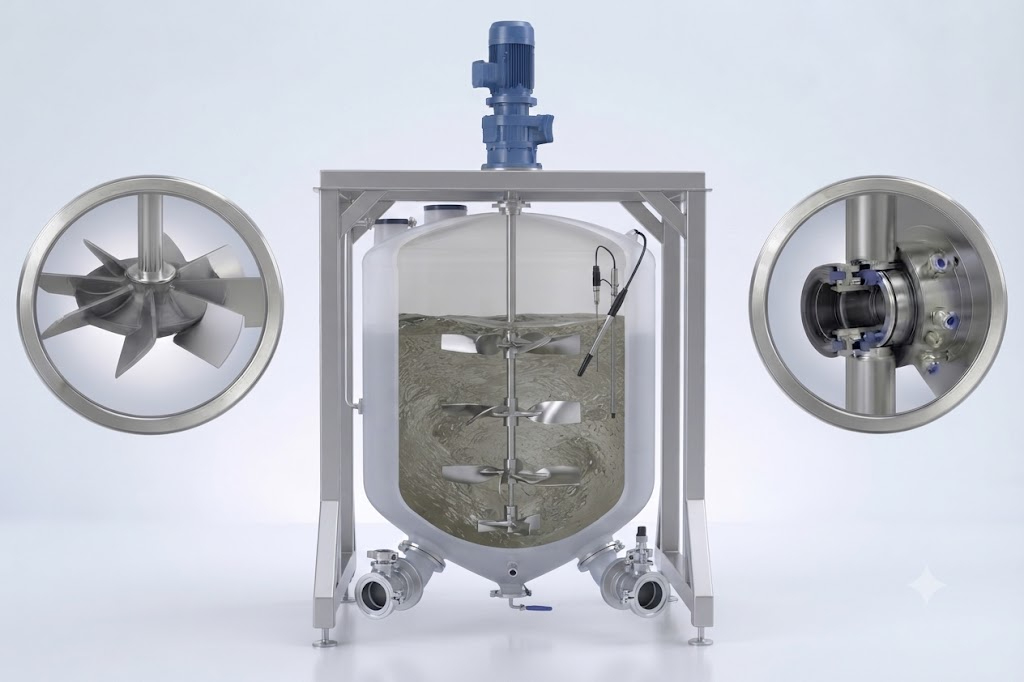
Agitators for Starch Processing Tanks
We offers a range of high-performance Agitators for Starch Industries, specially designed to optimize the processing and extraction of starch from various raw materials such as maize, wheat, and potatoes. Our agitators are engineered to handle the unique challenges of the starch manufacturing process, ensuring efficient mixing, superior product consistency, and energy savings across critical stages of starch production. From fiber washing to gluten separation, our agitators guarantee the highest standards of operation, making them the preferred choice for starch production facilities globally
Get Your Free Quote…!
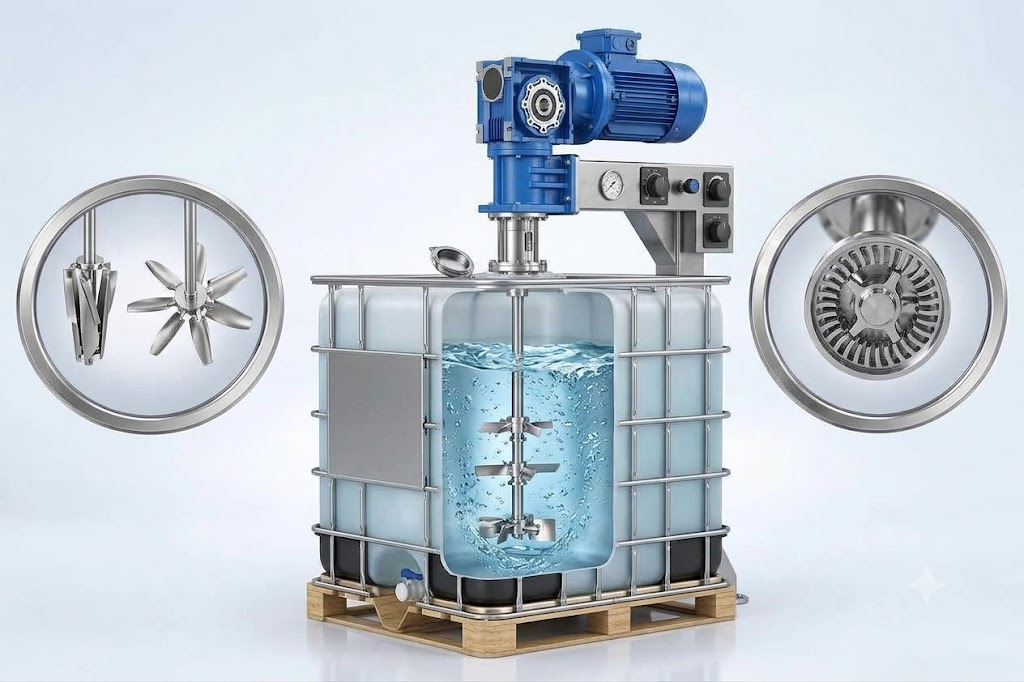
IBC/Tote Tank Mixer
our IBC/Tote Tank Mixers are designed to provide efficient mixing solutions for Intermediate Bulk Containers (IBCs) and Totes, ensuring that even high-viscosity liquids or challenging mixtures are properly blended. These mixers are engineered to cater to various industries such as chemical processing, food and beverage, pharmaceuticals, and agriculture, where uniform mixing is essential for maintaining product quality and consistency.
Get Your Free Quote…!
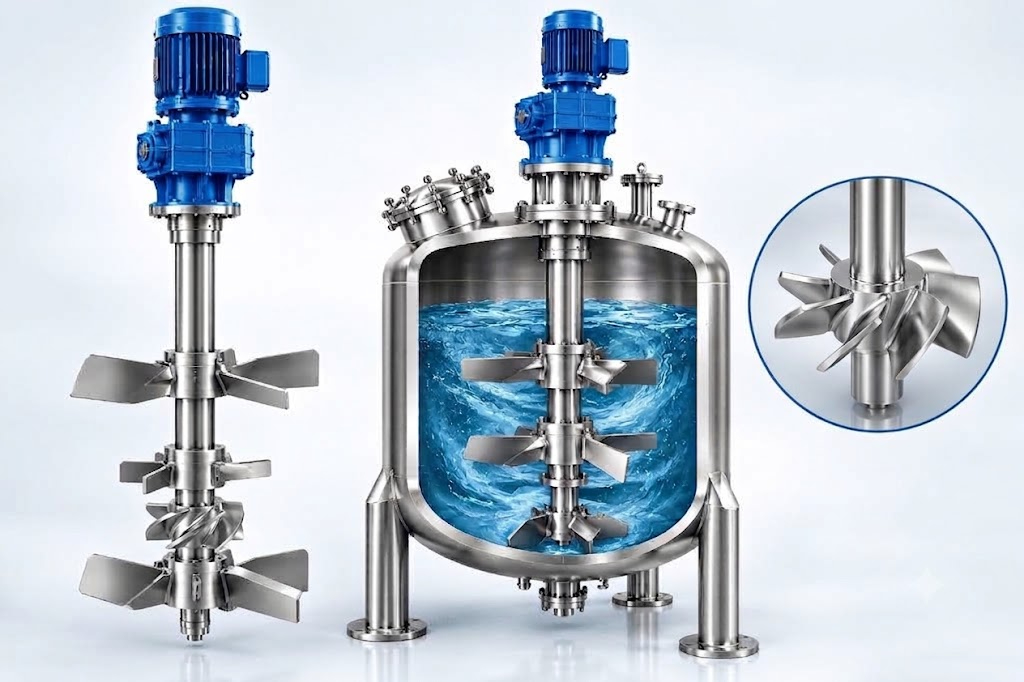
Reactor Agitator
The reactor agitators are the most powerful agitators compared to the others in our product range.
These Agitator are specially designed to serves the purpose of facilitating the chemical reaction, which is carried out with precise and meticulously calculated reaction times for which vigorous stirring is required.
Since the reactors operates at high temperature and pressure for this reason, mechanical seal is often installed to maintain constant pressure or prevent the internal dangerous Liquid/gases from dispersing.
Get Your Free Quote…!
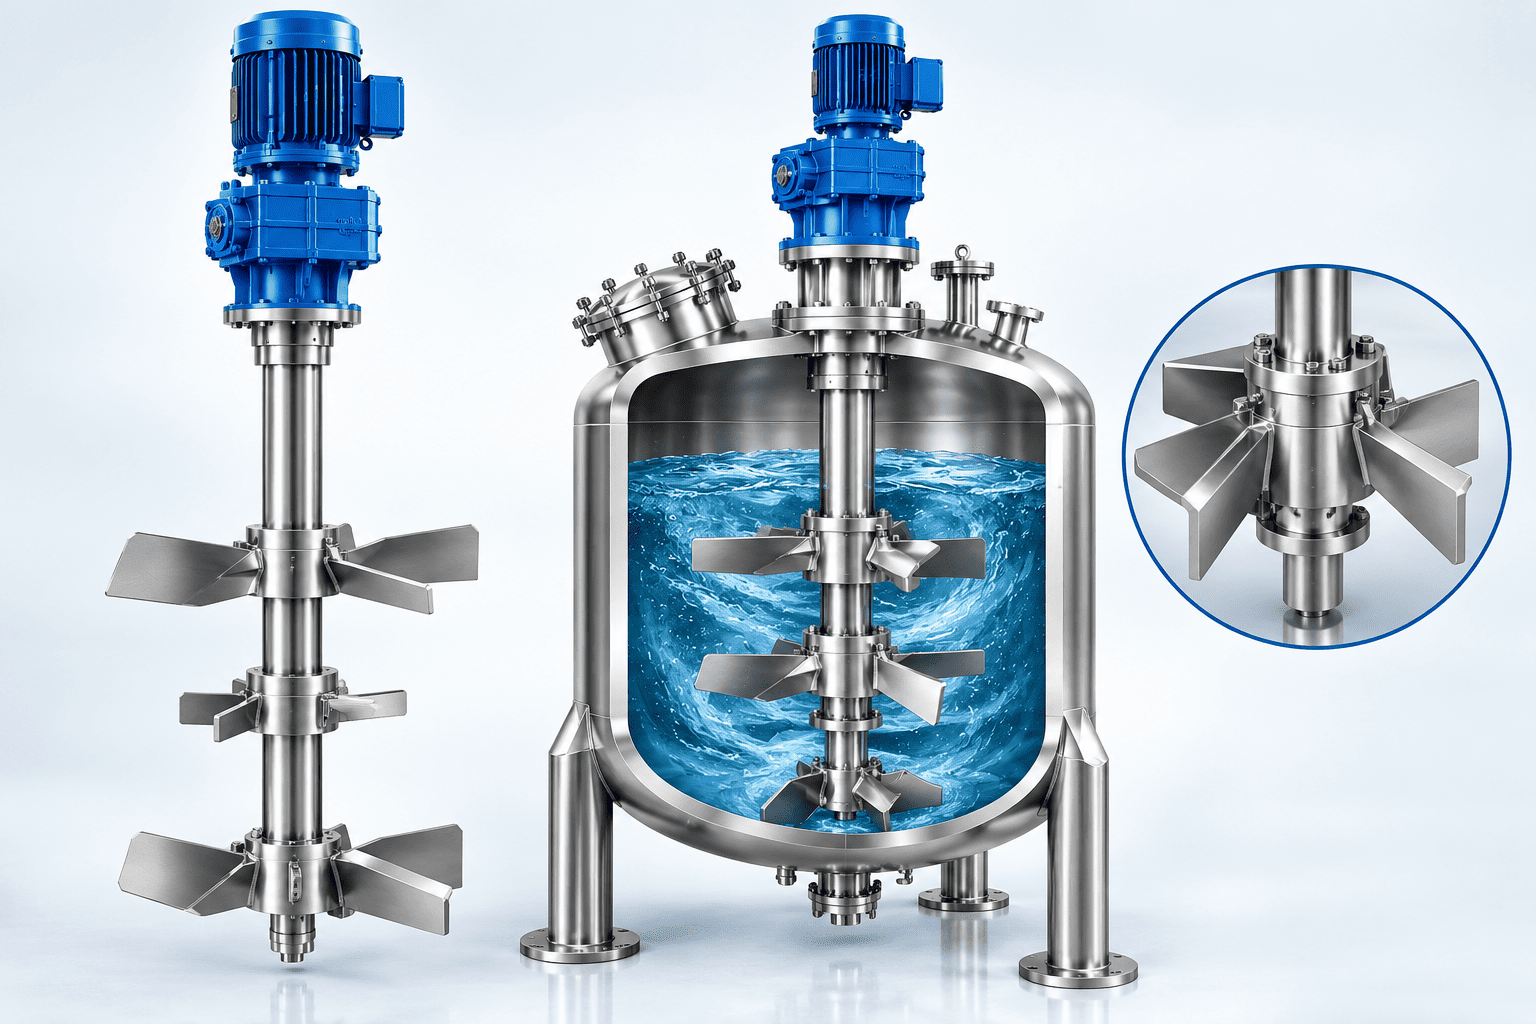
Heavy Duty Agitators
Heavy Duty Agitators are designed for large volume Vessels which are reliable for most demanding heavy industrial applications, from pharmaceutical fermentation, hydrogenation, bio digesters, chemical reactors, resins, large-scale chemical processing to minerals processing and heavy sludge waste treatment.
Radial and axial loads on the drive are completely absorbed by a separate double bearing section and the flexible coupling connecting the mixer shaft to the drive. These Heavy Duty Industrial mixer has a rigid torsion-free Bearing housing.
This robust construction and the precision of its running characteristics guarantee the durability of the shaft.
Get Your Free Quote…!
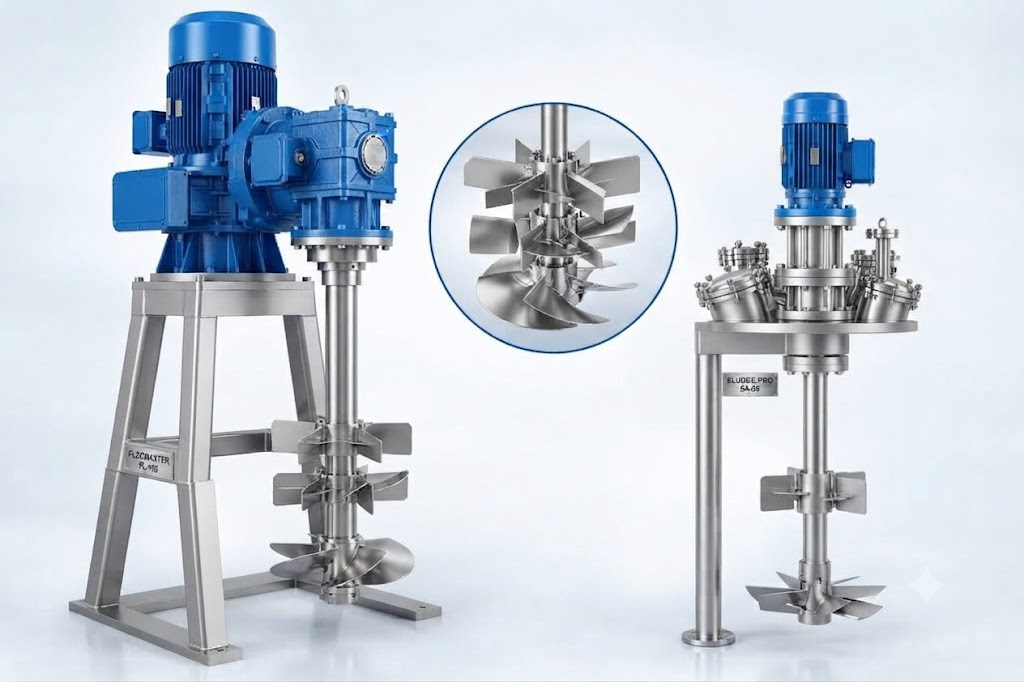
Flocculators Sludge Agitators
Flocculators provides gentle agitation by slow moving paddles. This action serves to break up the mass rotation of liquid and promote mixing.
The specially designed flocculating paddles enhance flocculation of the feed solids. Low tip speeds create a gentle rotary mixing which promotes floc development. Increased particle contact will promote floc growth and aids faster settling
Low tip speeds provide gentle mixing and minimize shearing action on established floc. Flocculators of various sizes and material of construction are available as per the application.
Get Your Free Quote…!
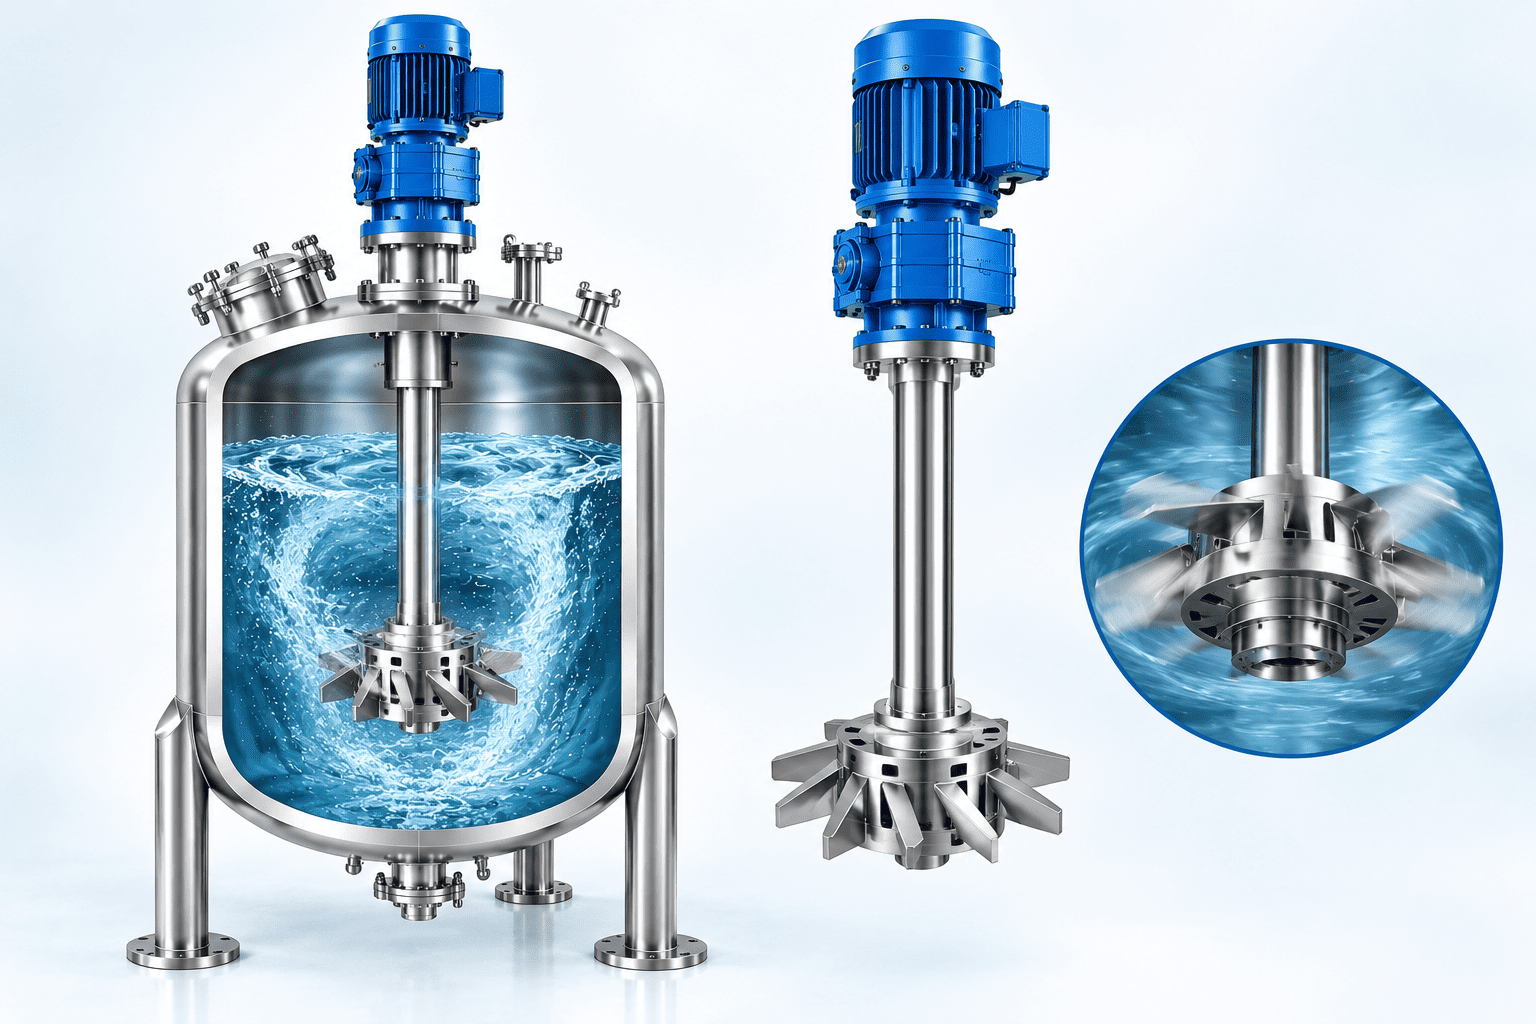
High Speed Agitators
Agitator type is an innovatively designed top flange agitator for use in the food and pharmaceutical industries. It is a mixer without gearbox, so there is no oil/lubricants leakage which could contaminate your product The mixer shaft is directly fitted directly into the drive, eliminating the need for an extra shaft coupling. The High- Speed Agitator are a strong and practically maintenance-free mixer which makes it a perfect solution for applications in the food and pharmaceutical industry. It is suitable for frequency converter-controlled operation.
Get Your Free Quote…!
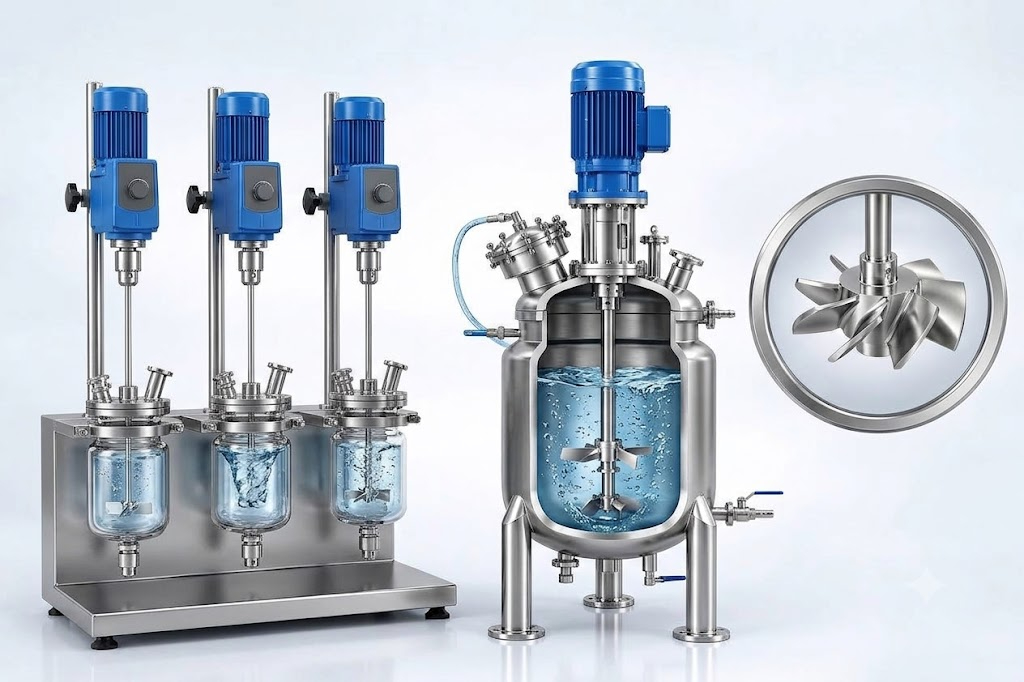
Agitators for small volume
Light duty top entry agitators are the best fit for applications with small volume tank like Coagulation, WTP, ETP, yeast fermentation, starch storage, storage and blending of concentrated fruit juices, bitumen, paint production, sanitary or pharmaceutical applications and many more.
This design of mixer which operates at speeds in range of 60-250 rpm is very suitable for mixing of different liquids, dissolving of solids in liquid, dispersion, Homogenous and emulsifying duties.
Get Your Free Quote…!
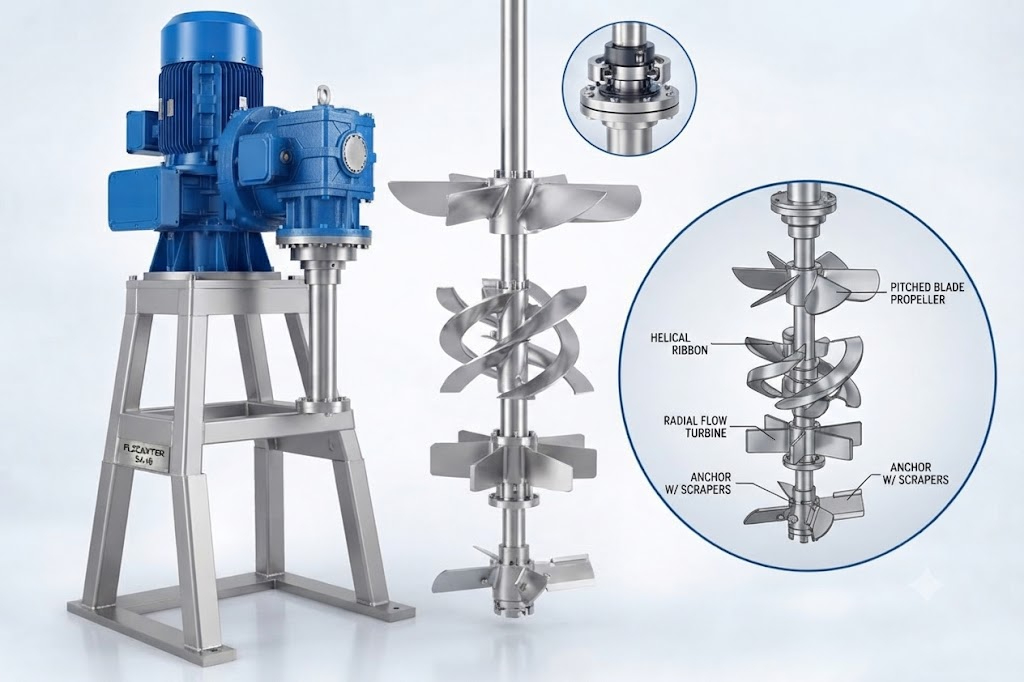
Mixing Impeller
Over the past few years, the demands for Mixing systems in industrial uses have consistently risen. Thus, We offers diverse range of mixing impellers designed with distinct performance attributes to fulfill a variety of application needs. The design of the Impeller blades, the choice of an appropriate mixing setup, and the arrangement of the agitator parts have a significantly impact both the process-related and mechanical characteristics. Each of our impellers are manufactured with 316 Stainless Steel material as the standard option. However, we also have alternatives such as 304 Stainless Steel, Mild Steel/Carbon Steel, Hastelloy, Titanium, and other premium alloy versions for most impeller designs as per the application. We also offer various surface treatments like polishing, coatings, and pickling and passivation processing.